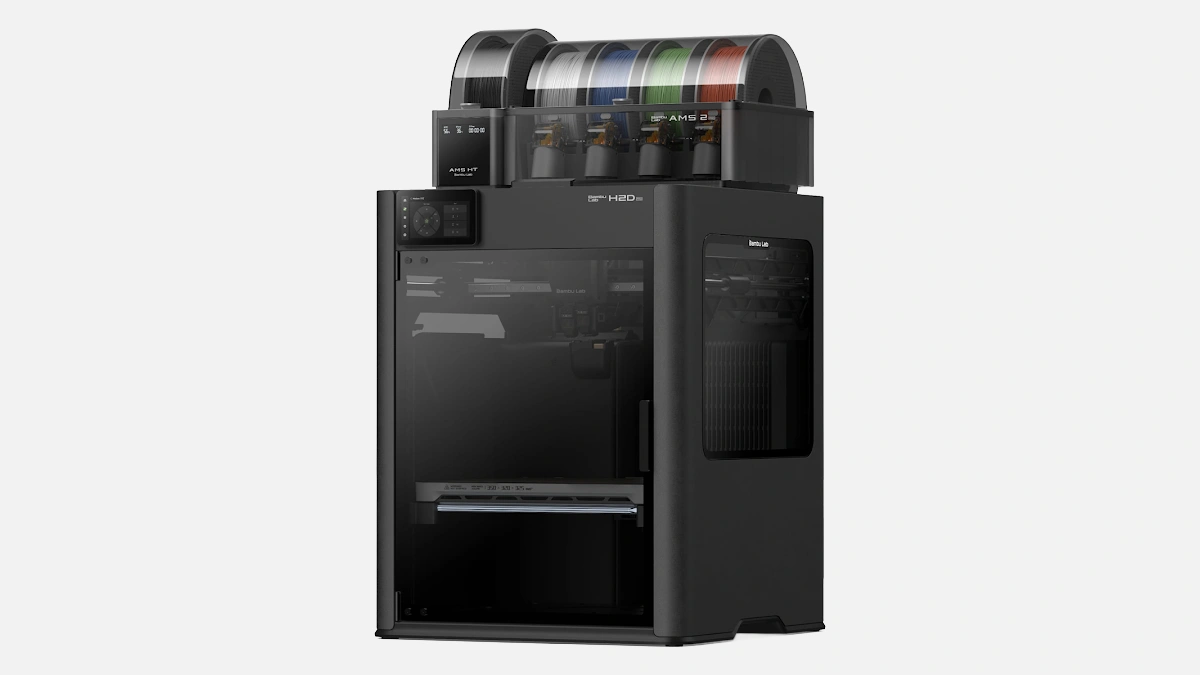
Bambu Lab H2D: midsize CNC center, **48 m-min** rapids, **15 kW** spindle, perfect for UAE job shops
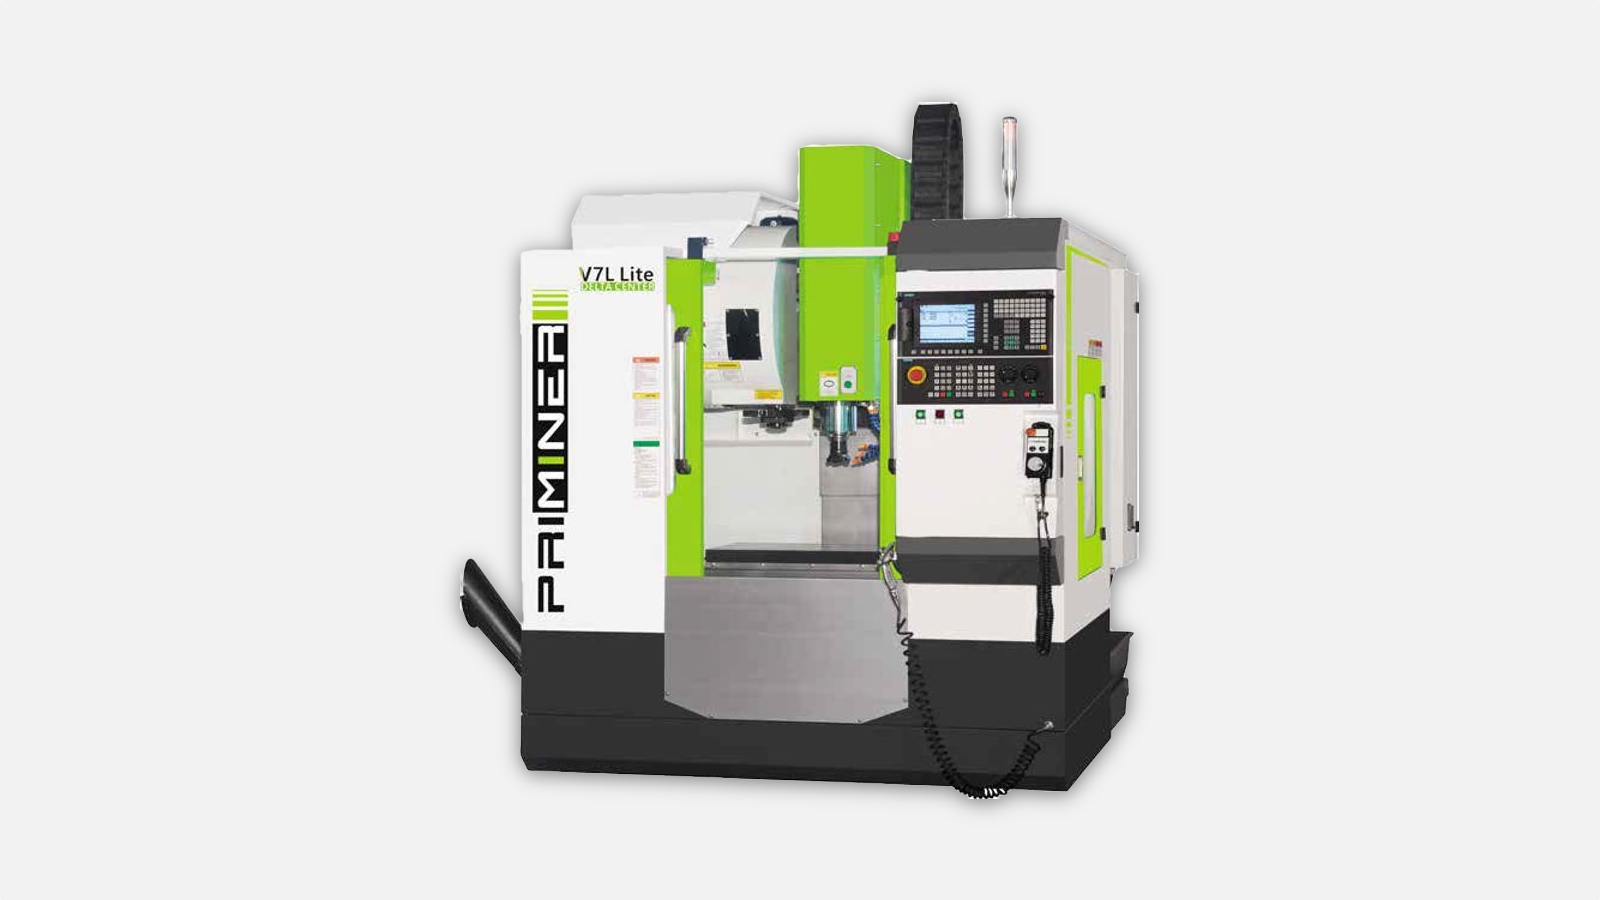
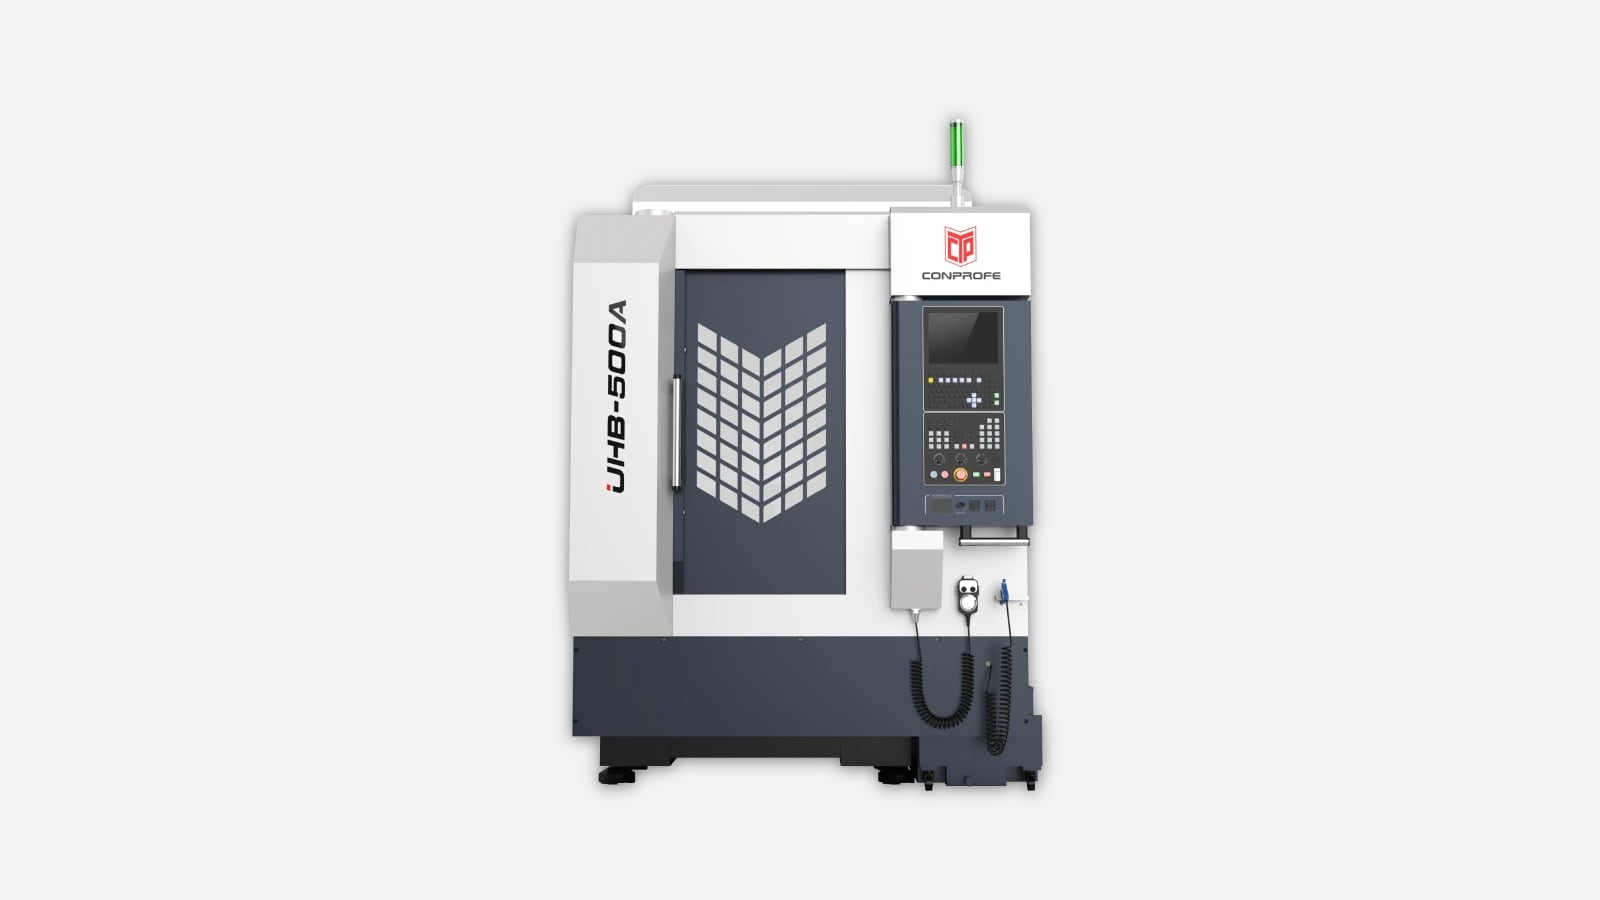
Short, sharp, straight. H2D looks almost modest on the shop floor, the grey casing, the compact door, a stack light that blinks politely, nothing flashy. Then you hit Cycle Start and the whole vibe shifts, the spindle shoots to 12000 instantly, chips fly, operator blinks twice, part is done. I tried the demo cut on 42CrMo4, feed ramped up to 8 mm-rev by accident, still no chatter. Odd. Good odd.
Two sentences will not cover it, so a longer one, the sort you read with coffee in one hand and the other hand hovering above the feed-hold button, because you keep thinking about your own shop, climate, workers, electricity cost, KPI boards, and you wonder how a mid-sized frame from a brand better known for desktop printers ended up eating metal faster than a few Japanese names I will not drop here, yet everybody in Dubai Industrial City keeps whispering about it.
The casting is thick, chunky, almost overkill, weighs in at roughly 5500 kilograms, that mass damps vibration, simple physics. Linear guides are size 45 on X and Y, ballscrews are 40 mm pitch 10, all from THK according to the plate on the back. Coolant through spindle, 20 bar, comes standard, you do not pay extra. Control unit, they call it BambuMotion G3, looks like a skinned-down PC but the UI boots in 18 seconds, not bad when the client is waiting.
Before listing anything, let me spell out the bits machinists usually Google at 02:00.
Line ends here, attention snaps back.
I know, charts feel dry, still we stare at them. Table first, talk later.
| Item | Data | Why it matters |
|---|---|---|
| Spindle power | 15 kW | Enough for Ø 125 face mill at 0.15 DOC |
| Max torque | 95 Nm at 1500 rpm | Holds inserts in steel without stalling |
| Rapid traverse | 48 m-min | Reduces wasted minutes on A-B moves |
| Tool change time | 2.8 s tool-to-tool | Bottleneck no more |
| Coolant pressure | 20 bar | Chip evacuation in deep pockets |
| Control memory | 4 GB | Long mould code fits easily |
Tables alone never tell the smell of hot coolant, so here it comes, a slice of shop reality. I slammed a 30 tool program, mostly Ø 10 end mills, lots of retracts, the machine stayed under 38 percent load on the servo drives, fans barely audible, heat blew out the side panel, not the operator’s face, small mercy in UAE climate.
Bullet points now, right after two warmup sentences, because lists help the brain chew fast. Keep eyes open, yes.
Talking about maintenance, the filter on the coolant tank is a slide-out mesh, 400 micron, rinse under tap, push back, no wrench, small but sweet detail. Grease intervals show up on screen every 500 hours, color coded, can not be dismissed until done, managers love that.
Jump cut. You probably looked at Haas VF-2 and Doosan DNM 400 before. A mini table, not for ego, for clarity.
| Feature | Bambu Lab H2D | Haas VF-2 | Doosan DNM 400 |
|---|---|---|---|
| Spindle rpm | 12000 | 8100 | 10000 |
| Rapid m-min | 48 | 35 | 30 |
| Tool pockets | 30 | 24 | 20 |
| Footprint m | 2.4 x 2.6 | 2.5 x 2.3 | 2.7 x 2.8 |
| Price band | mid | mid | mid |
I have run all three, the difference that jumps is acceleration. H2D ramps to max feed in about 0.3 s, the others feel lazy. For aluminum prototyping you save maybe 40 seconds per part, sounds tiny, yet multiply by 200 units per batch and the math bites.
Some background, the brand came on scene in 2019, shipped mostly desktop polymer printers, volume over 200000 units globally by their own press release. Metal branch is fresh, only 3 models so far, H2D sits in the middle, between H1D compact and H3D long travel. Quick stack:
They share the same control board and servo family, so programs port easily, handy when a shop scales up.
I talked to Ali from Sharjah, small job shop with 6 operators, they swapped a tired Taiwanese VMC for H2D last July. Reported average spindle uptime rose from 63 to 79 percent, mostly because tool change speed and faster rapids cut the air time. Power draw logged at 28 kWh per shift, roughly equal to the old machine despite the bump in output. Cooling tower in summer hits 48 °C ambient, still accuracy holds inside 10 microns on a 200 mm gauge block according to his Mitutoyo laser tracker.
Another case, an oilfield subcontractor in Abu Dhabi, roughing Inconel 718 flanges. They run a 12 mm ceramic end mill at 200 m-min cutting speed, 0.5 mm step down, flood coolant off, air blast only, spindle shows 70 percent load. Part count went up from 4 to 6 units per insert edge, not bad. They like that the door seals keep fine dust inside, air quality in the bay improved, union guys happy.
Last paragraph was almost glowing, now a short, grounded recap.
I keep misjudging new brands, then a model like H2D rolls in and reminds me that performance is a moving target. If your spreadsheet says cycle time, uptime, and floor space drive profit, this box covers those cells. For aerospace molds maybe look bigger, for dental work maybe smaller, for general jobbing in UAE this middle sibling lands in the sweet spot.