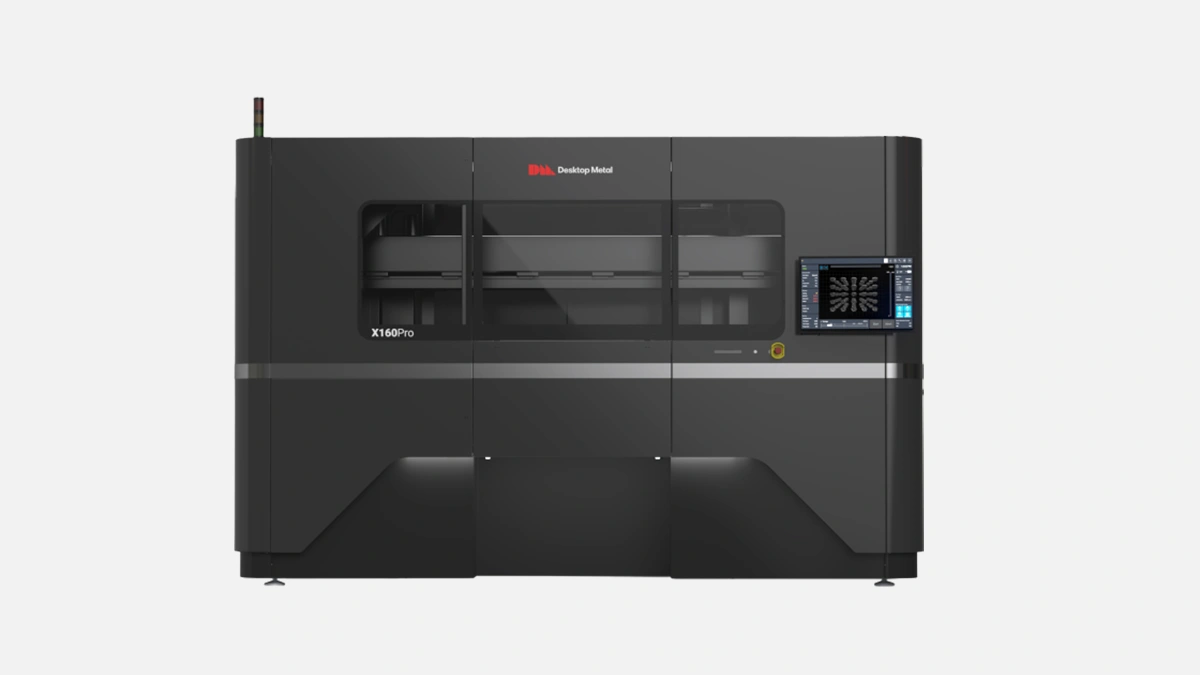
Binder-jet monster, 160 L build, pushes 10 000 cm³ ⁄ h, perfect for UAE medium-batch metal parts
Big box, lots of noise. Powder jets everywhere. That is the vibe you get when the X160Pro lights up for the very first shift. You stand a bit aside because the recirculating powder cloud looks like it could repaint your overalls in stainless glitter. Cool though.
Then the numbers hit. 160 liters of packed powder, 10 000 cubic centimeters per hour, sometimes even more when the path planning is gentle. Those raw figures sting, almost like someone tells you your old laser printer has been jogging and got ripped.
Operators from Mussafah call, they want parts for oilfield valves, impossible geometries, strict lead times. They have gas but no time. Binder jetting is suddenly not a laboratory trick, it is a shop-floor tool, and Desktop Metal has been feeding that idea hard for 9 years already. Four generations of the X-series rolled out, each one less fragile, more shopable, you get the picture.
Before diving into chatter let us lock a few facts.
| Item | Figure | Why it matters to you |
|---|---|---|
| Build box | 800 × 500 × 410 mm | Fits pump casings in one pass |
| Native resolution | 1600 dpi | Edges stay sharp on fine lattice |
| Pass rate | up to 350 layers per hour | High layer count without night shift |
| Average powder reuse | 97 % | Cuts raw material spend in Dubai |
| Typical sinter shrink | 18–20 % isotropic | Easy to compensate in CAD |
| Max qualified density | 7,7 g / cm³ for 17-4PH | Meets NORSOK M-650 class 1 |
The table is dry, sure, but it keeps discussions focused. Nobody likes vendor brochures with fuzzy adjectives.
Before the list comes a small confession. I first saw the X160Pro at Formnext, stood half sleepy, the coffee was cold, still the printer grabbed attention because of that conveyor vibe. Parts in at one end, green bricks out the other, no drama.
Those points look random yet they are the bits people actually DM on LinkedIn at midnight.
A second list coming at you, brace.
Back to paragraphs.
Desktop Metal ships three boxes under the X label. The baby X25Pro, the middle X160Pro, the cargo-plane X390Pro. Same printheads, same binder, only the sandbox scales. The 25 gives you 16 liters, cute for dental arches, the 390 eats 300 liters and therefore space. The 160 feels like the Goldilocks zone, one man can load it, one forklift can move it, and the sinter furnaces you already run for MIM pucks will swallow its build plates. Switching among models means you keep your material parameters which is a silent cost saver.
People love to pit Desktop Metal against ExOne, HP Metal Jet and the Chinese newcomers. Let us do it quickly. ExOne InnoventX is super precise, but the build is 19 liters, a toy for labs. HP Metal Jet is fast, no doubt, yet the binder chemistry is proprietary and the furnace list is short. An open binder plus third-party furnace compatibility remains a calm argument for the X160Pro. Chinese machines like EPlus EBJ300 cut price, still struggle with spare parts in the GCC, your CFO will notice downtime more than upfront savings.
Desktop Metal qualifies powders in batches, ASTM certificates on their site, no paywall. Stainless 316L, 17-4PH, tool steel H13, Inconel 625, pure copper. AISI 4140 is in beta, rumors say Q4. UAE oil service companies keep asking for duplex, agency says development ongoing, fingers crossed.
Two options on tap. Phenolic for steels, water-based for copper. You switch a cartridge, flush lines, done. No acid smell, exhaust passes through a simple charcoal bed. In Ras Al Khaimah one customer installed the printer inside an air-conditioned bay next to CNC lathes, only added a cheap fume hood, neighbors never complained.
Let us do a crude Friday afternoon calc. A stainless impeller weighs 1,4 kg sintered, packing density in the box hovers around 55 % for that geometry, so one full bed gives roughly 63 finished wheels. With average cycle time 17 hours print plus 25 hours furnace you pump 2,3 beds per week, round it to 140 parts. A milling shop in Sharjah doing the same wheel needs 4 five-axis machines, eight operators and cries each time the hub angle changes. Binder jetting laughs at angle changes, you only re-slice.
Printer itself sips 7 kW peak, mostly on heaters and pneumatics. Furnace is the real hog, 85 kW during ramp, UAE power is relatively cheap compared to Europe so the electrical bill rarely scares managers. Bonus, no argon blanket, nitrogen is enough for steels which is trivial to source.
Desktop Metal offers on-site service hubs in Dubai Investment Park for 48 h response. Users can still swap printheads solo, eight screws, plug, align via onboard camera. Annual preventive kit costs less than a spindle rebuild on a turn-mill so bean counters tend to nod.
Ahmed from Al Ain texted last week, said he banged out 11 000 green parts in three months, only one misfire due to clogged nozzle after running recycled copper with big agglomerates. He sieved finer next batch, problem gone. That anecdote teaches more than polished PR.
Desktop Metal was founded in 2015, Massachusetts, now over 500 employees, they absorbed ExOne in 2021, total printer output around 1200 units per year across all lines. The X160Pro itself sits at revision C, firmware 4.3.6 at the moment of writing.
Oil and gas service contractors, aerospace MRO shops in Dubai South, even a jewelry casting house that sneaks copper cores for rubber molds. Pattern is simple, anybody with medium batch sizes, tricky channels inside parts, and a furnace already on site sees advantage.
Speed without lasers, open materials, footprint a forklift can digest. These three items stay with you after the sales demo. You can hate the slightly plasticky door hinge or the fact the touchscreen prefers clean gloves, still the parts keep rolling out. That rhythm ultimately convinces production managers more than buzzwords.