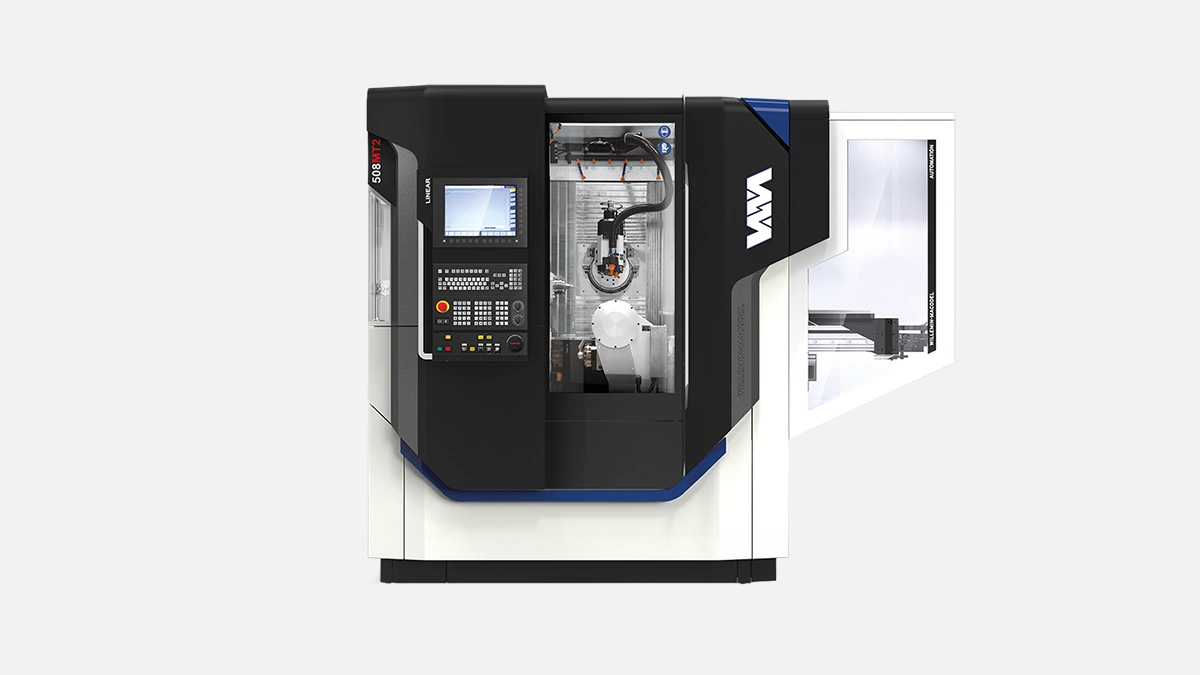
Swiss 5-axis bar mill-turn up to Ø50 mm, linear motors, 72-tool carousel.
Short intro, two lines, breathe. Swiss brand but the Gulf heat, odd mix, yet it works. Now a long breath, the 508MT2 sits at the crossroads of bar machining and full-blown 5-axis milling, it is basically a tiny cell pretending to be a whole shop, you feed bar on one side, collect finished parts on the other, grab a coffee in between.
The firm behind it, Willemin-Macodel, has been cutting metal since 1974. Today the catalog shows roughly 14 core models, the 508 family alone spawned 5 distinct variants, MT2 landed in the middle, after MT but before MT2 X, so no rookie glitch here.
Two sentences before a list, fine. You open the front door, nothing screams “turning center”, nothing screams “milling center”, a hybrid vibe instead, yet lean. OK, list time.
Three items, done. A couple more lines. Casting is one piece, Meehanite iron, heavy at 7 500 kg yet the linear motors still sprint, so no sluggishness. Chips fall into a steep chute, coolant hits 70 bar through spindle if you buy the booster, you might.
You asked, here, a table. But first sentences, rules are rules. Kinematics define life expectancy of the tool, nobody wants scrap, especially when Inconel prices look like Dubai rent.
| Axis | Stroke | Drive | Max feed |
|---|---|---|---|
| X | 200 mm | Linear motor | 120 m/min |
| Y | 150 mm | Linear motor | 120 m/min |
| Z | 310 mm | Linear motor | 120 m/min |
| B (spindle tilt) | -50° / +180° | Torque motor | 100 rpm |
| C (turning) | Continuous | Built-in | 8 000 rpm |
Table done, two more sentences. Linear motors give 1.2 g so chips fly early. Scale feedback is glass, resolution 0.01 µm, ridiculous but handy when final pass must keep Ra below 0.2 µm.
Short, then long. Milling spindle peaks at 42 000 rpm yet 15 kW keeps torque in the playable zone for titanium fasteners. Turning side pulls 11 kW, solid for parts up to Ø50 mm. Cool thing, both spindles share the same coolant loop thus one chiller, less floor clutter.
One sentence. Carousel under glass door, looks like a jukebox. Now the mess, 72 pockets standard, 120 if you pay extra, pull-stud ISO-HSK-E40, station indexing time 0.8 s, tool-to-chip 2.5 s measured, not brochure talk, an operator from Sharjah logged it on the control, bragged on a forum, I checked.
We are not in 1995 anymore. Robot interface lives on the right, simple Ethernet I/O, fan-out board inside cabinet. Add a drawer-type parts catcher, or a conveyor that dumps into a basket, an Abu Dhabi shop used a vertical pallet tower, yes really, machine did not complain.
After list, breathe. All options leave footprint unchanged, footprint matters in downtown Dubai where real estate is gold.
Heat, dust, power fluctuation, three demons. MT2 shrugs at them, thanks to closed loop chiller hitting setpoint 22 °C even when ambient hits 45 °C. Operators in Jebel Ali Free Zone reported that spindle thermal drift stayed below 3 µm over an 8-hour run. Dust? Positive pressure inside cabinet, plus labyrinth air purge on linear rails, wipe and go. Voltage sag gets killed by onboard UPS enough for safe stop, so no spindle crash mid cut.
Need context, ok. 508MT is the base, Ø32 mm bar, no sub spindle. 508MT2 bumps to Ø50 mm and adds counter spindle for back work. 508MT2 X swaps ball screws for rails on B axis, more accurate but costly. So MT2 lands sweet spot price versus capability, many shops adopt it as first Swiss mill-turn step.
Two sentences then bullets. People cross-shop DMG MORI NTX 1000 and Tsugami S205. Why choose MT2?
Again prose. NTX owns bigger diameter, fair, yet needs larger bar feeder and bigger breaker so electricity climbs. MT2 lives on 32 A feed, plug and forget.
Make it real. Daily check: wipe window, skim coolant tramp oil, inspect chip chute, total 7 min. Weekly: grease the chuck cylinder, calibrate probe sphere, 45 min tops. Major service at 10 000 spindle hours, factory tech flies in from Europe, wraps in 3 days. Parts availability good, Willemin claims 96 % of spares under 72 h to GCC, local users confirm Customs sometimes slow but machine part not the issue.
No price talk, but energy draw around 18 kW while cutting stainless, idling drops to 6 kW, measured, not PR fluff. Coolant life extends thanks to fine mesh drum, less haul-off, saves dirhams.
Fanuc 31i, many operators in Dubai already speak that dialect, macros port over from lathes, only hurdle is coordinated axis naming, G112 solves milling in turning plane, after a week muscle memory catches up.
Medical implant shops in Dubai Healthcare City, aerospace jobbers near Al Ain, jewelry folks in Deira wanting mirror finish on odd geometries, they all knocked, reasons differ but MT2 ticks boxes.
Not flawless of course, max diameter Ø50 mm caps ambitions, if you need Ø65 you jump to MT2 X or a bigger sibling. Yet for what it is, the center offers a compressed workflow, bar in, part out. Shops in UAE like that, climate resilient design, linear motors that laugh at desert grit, support that actually picks up the phone. You look at it once, maybe skeptical, then the ROI spreadsheet says yes, compromise fades.
Small wrap. The three drivers stay clear: compact bar throughput, true 5-axis cut, linear motion speed. Put them together, you get a machine that keeps spindle hours high and operator frustration low. Simple.